- Proudly Made in the USA
Choosing the best China Tower Clamp supplier requires more than comparing prices and catalog photographs. The decision affects structural safety, installation speed, maintenance, and long-term project reliability. A clamp may look excellent on a screen, yet fail your requirements through poor fit, inconsistent galvanizing, or incomplete testing records.
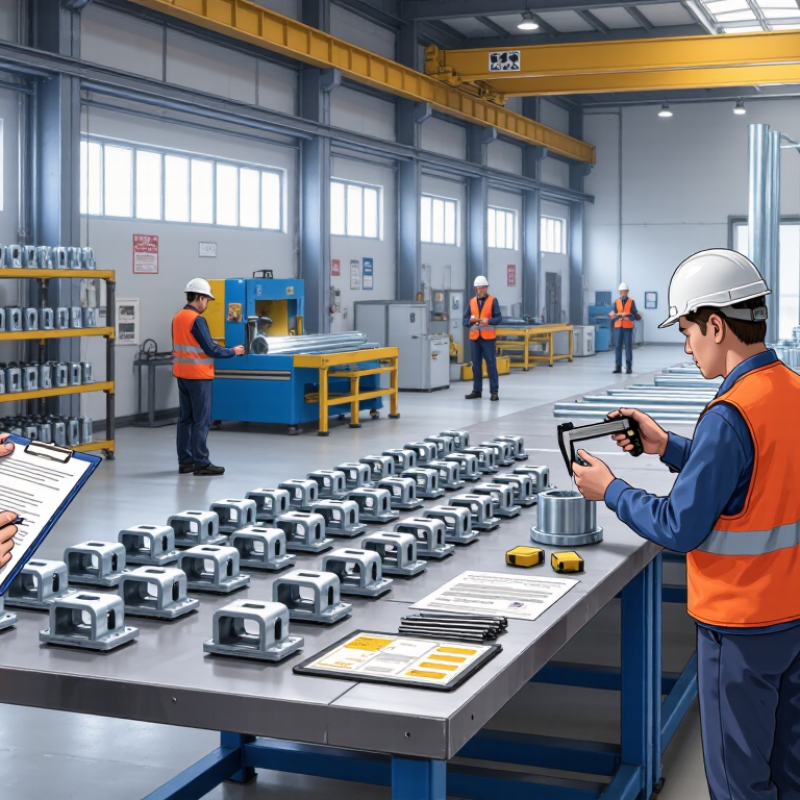
Liang Wei, a senior tower-inspection engineer, offers a practical reminder: “A reliable clamp begins with verified steel, accurate dimensions, and documented testing.” His point is simple. Supplier evidence matters. Request material certificates, load-test reports, coating specifications, dimensional drawings, and batch traceability. Ask how the factory controls bolt quality, welding, thread accuracy, and surface protection. If possible, inspect production areas and review samples before placing a large order.
Experience also matters. A capable manufacturer should understand tower angles, tube diameters, antenna mounting loads, wind exposure, and field installation limits. The best supplier will ask technical questions before suggesting a product. That is a good sign.
Do not trust claims blindly.
A low quotation may reduce immediate costs. It may also conceal weaker steel, uncertain tolerances, or expensive rework. However, a higher price is not automatic proof of quality. This is where careful comparison becomes necessary. Evaluate engineering support, communication, delivery records, inspection procedures, and after-sales response together. Some evaluations remain imperfect because project conditions differ. That is normal. A responsible buyer keeps questioning assumptions and verifies critical details before approval.
How to Choose the Best China Tower Clamp Supplier?
Define Tower Clamp Requirements for Your Project
A reliable purchase begins with a clear tower clamp specification. Describe the tower type, pipe diameter, connection method, and expected load. Include both static loads and movement caused by wind. Small details matter.
State the required material, surface finish, and operating environment. Galvanized steel may suit outdoor towers, but coastal projects need stronger corrosion protection. Check temperature ranges, drainage needs, and contact with dissimilar metals. Do not assume one clamp design fits every structure.
Provide drawings with dimensions and tolerance limits. A supplier should confirm bolt sizes, hole positions, thread quality, and tightening requirements. Ask for material certificates, load test records, inspection reports, and traceability documents. Independent testing can add confidence when the application carries serious risk.
Request production samples before approving a large order. Measure the sample yourself, including hole alignment and coating thickness. Factory photographs help, but they never replace physical inspection. A spreadsheet can still miss a poor weld. I have learned that unclear drawings create expensive corrections later.
Discuss packaging and delivery conditions, especially for large quantities. Confirm how parts remain protected during transport and storage. Keep a written record of every revision. Clear requirements make supplier comparisons fairer and reduce avoidable disputes.
Define clear tower clamp requirements before comparing suppliers. The example below uses a 100-point project evaluation model that prioritizes structural safety, material traceability, corrosion protection, dimensional fit, documentation, and delivery reliability.
How to use this chart: Ask each supplier to provide test reports, material certificates, coating records, dimensional inspection data, and delivery commitments that match the weighted requirements of your project. The final clamp selection should also be verified against the applicable tower design calculations and standards.
When choosing a China tower clamp supplier, inspect production evidence, not only catalog photos. The World Steel Association reported 1.89 billion tonnes of crude steel production globally in 2023. China produced about 1.02 billion tonnes. This scale does not guarantee consistent clamp steel. Ask for heat numbers, mill certificates, and batch traceability. A capable factory should connect each lot with incoming inspection, forming, welding, heat treatment, and final release. Walk the production line if possible. Check calibrated torque tools, load-test fixtures, coating gauges, and controlled storage. A polished factory tour can still mislead. Check records.
Product quality needs measurable proof. Request dimensional reports, hardness results, slip-load tests, and tensile data from normal batches. For hot-dip galvanized clamps, verify coating thickness and adhesion, not just surface brightness. The NACE IMPACT Study estimated global corrosion costs at US$2.5 trillion annually, or about 3.4% of global GDP. Corrosion control is not cosmetic. Confirm steel grade, bolt property class, thread accuracy, and washer fit against approved drawings and applicable standards. Samples should come from routine production, not specially prepared units.
Audit nonconformance handling too. Ask for rejected-part rates, corrective-action reports, calibration dates, and record-retention periods. Good suppliers explain failures without defensiveness. They should provide a pre-shipment inspection plan and batch-linked photographs. One limitation remains: small samples can miss hidden variation. Repeat testing after production changes. Price matters, but weak process control creates rework, site delays, and early replacement. Documentation may look excellent while factory discipline remains weak. Verify both.
Choosing the best China tower clamp supplier requires more than comparing prices. Start with material evidence. The World Steel Association reported 1.892 billion tonnes of crude steel production in 2023, showing the scale of global steel manufacturing. Scale alone proves nothing. Request mill certificates, heat numbers, chemical composition, tensile strength, and coating thickness for every production batch. Match these records against the specified grade, such as structural carbon steel or stainless steel.
Check applicable standards carefully. Tower clamps may need testing against project specifications, ASTM requirements, EN standards, or telecommunications tower criteria. Ask whether dimensions, bolt torque, slip resistance, and ultimate load capacity were verified by an independent laboratory. A credible supplier should provide test procedures, sample identification, calibration records, and complete reports. Photos help, but they are weak evidence.
The ISO Survey of Management System Standard Certifications consistently records more than one million ISO 9001 certificates worldwide. Yet certification does not automatically guarantee reliable clamps. Visit the factory, inspect stamping, thread quality, welds, and galvanizing marks. Watch a sample inspection, not only a presentation. Traceability matters. Each carton should connect to a batch, drawing revision, and inspection result. Ask difficult questions.
Suppliers sometimes provide polished documents with missing test conditions. That is a warning. Also, coating thickness can vary around sharp edges and bolt holes; one measurement is insufficient. I would recheck critical samples, because even a well-written specification can miss real installation conditions.
| Evaluation Dimension | What to Verify | Relevant Standard or Reference | Acceptable Evidence | Recommended Benchmark | Warning Signs |
|---|---|---|---|---|---|
| Base Material | Confirm the steel grade, chemical composition, mechanical properties, and traceability of the raw material used for the clamp body. | GB/T 700 for Q235 structural steel; GB/T 1591 for Q355 structural steel; ASTM A36 may be specified where applicable. | Mill test certificate showing heat number, grade, chemistry, yield strength, tensile strength, and elongation. | Material grade and certificate data must match the approved drawing and purchase specification. | Generic certificates, missing heat numbers, or certificates that do not identify the supplied batch. |
| Fastener Grade | Check bolt, nut, and washer grades, dimensions, thread type, and compatibility with the clamp body. | ISO 898-1 for carbon and alloy steel bolts; ISO 898-2 for nuts; ASTM F3125 may apply to specified structural bolts. | Fastener test report, grade marking, dimensional inspection record, and batch traceability documentation. | Fasteners must meet the specified property class and be supplied with compatible nuts and washers. | Unmarked fasteners, mixed property classes, damaged threads, or substitution without written approval. |
| Corrosion Protection | Verify hot-dip galvanizing or other coating type, coating thickness, surface preparation, and post-treatment. | ISO 1461 and GB/T 13912 for hot-dip galvanized coatings on fabricated iron and steel articles; ASTM A123 may be specified for structural steel products. | Coating thickness report, visual inspection record, galvanizing batch information, and repair procedure for damaged areas. | Coating thickness must meet the applicable standard and project requirement; the surface should be continuous and free from serious bare spots or excessive zinc build-up. | No coating records, severe bare areas, peeling, heavy ash deposits, blocked threads, or unapproved paint repair. |
| Dimensional Accuracy | Check hole diameter, center-to-center distance, plate thickness, bend radius, clamp opening, and overall dimensions. | Approved engineering drawing, purchase specification, and applicable general tolerances such as ISO 2768 where specified. | Inspection and test plan, calibrated measuring-tool records, first-article inspection report, and sampling inspection results. | All critical dimensions should conform to the approved drawing and stated tolerances before shipment. | Measurements taken without calibrated tools, undocumented changes, or dimensions checked only after customer complaints. |
| Load Capacity | Confirm the intended load direction, proof load, ultimate load, slip resistance, and safety factor for the tower application. | Project-specific structural calculations and applicable tower design requirements; do not rely on a generic catalog load rating. | Signed calculation, test method, test fixture description, load-displacement data, photographs, and independent laboratory report when required. | The rated capacity must be supported by calculations and physical testing using the actual clamp configuration. | Load ratings without test conditions, unclear safety factors, or test results for a different model or material. |
| Mechanical Testing | Verify tensile strength, yield strength, elongation, hardness, and any required proof-load or destructive-load testing. | GB/T 228.1 or ISO 6892-1 for metallic tensile testing; GB/T 230.1 or ISO 6508-1 for Rockwell hardness where applicable. | Laboratory report identifying specimen location, test equipment, calibration status, test date, batch number, and results. | Testing should be performed according to a recognized method and linked to the actual production batch. | Reports without specimen details, missing calibration information, or results copied across multiple batches. |
| Corrosion Testing | Determine whether salt-spray or other environmental testing is necessary for the installation location and coating system. | ISO 9227 or ASTM B117 for neutral salt-spray testing; test duration must be defined by the project requirement. | Test plan stating exposure time, specimen preparation, test conditions, corrosion rating, and photographic records. | Use corrosion testing as supplementary evidence; it should not replace coating-thickness and visual inspections. | Unspecified test duration, unrelated coating samples, or claims that salt-spray hours directly equal service life. |
| Welding Quality | For welded clamps, verify welding procedure, welder qualification, weld size, visual quality, and non-destructive testing requirements. | ISO 3834 for quality requirements for fusion welding; ISO 5817 may be used for weld quality levels; project specifications may require additional standards. | Welding procedure specification, welder qualification records, weld inspection report, and non-destructive testing report when specified. | Welds should be free from cracks and unacceptable lack of fusion, undercut, porosity, or dimensional defects. | Unqualified welding personnel, undocumented repair welding, or welds covered by coating before inspection. |
| Quality Management | Assess process control covering incoming materials, production, inspection, nonconforming products, corrective action, and final release. | ISO 9001 quality management system requirements. | Current certificate issued by an accredited certification body, audit scope, quality manual or procedures, and sample inspection records. | The certificate scope should cover the manufacture of relevant metal or tower hardware products and remain valid during the order period. | Expired certificates, unverifiable certificate numbers, or certification scope unrelated to the supplied product. |
| Laboratory Competence | Check whether testing is performed by a competent internal laboratory or an independent laboratory with suitable accreditation. | ISO/IEC 17025 for competence of testing and calibration laboratories. | Laboratory accreditation certificate, scope of accreditation, equipment calibration records, and signed test reports. | Critical performance tests should be traceable to calibrated equipment and a laboratory capable of performing the stated method. | Laboratory reports with no accreditation scope, missing test method, or no equipment identification. |
| Production Traceability | Verify that raw material, forming, welding, galvanizing, inspection, packing, and shipment records can be linked to one batch. | Supplier quality plan and customer-specific traceability requirements. | Batch number, heat number, traveler or routing sheet, inspection release note, and packing-list references. | Each shipment should be traceable from finished product back to the raw-material heat and relevant inspection records. | Unlabeled cartons, mixed batches, handwritten records with unexplained changes, or no retained samples. |
| Sampling and Inspection Plan | Review inspection frequency, critical characteristics, acceptance criteria, and handling of rejected parts. | Customer-approved inspection and test plan; ISO 2859-1 may be used for attribute sampling when agreed by the parties. | Inspection and test plan, control plan, sampling level, acceptance number, inspection forms, and nonconformance records. | Critical safety dimensions and load-related features should receive defined inspection controls rather than relying only on random visual checks. | No acceptance criteria, unspecified sample size, or replacement of failed samples without documented investigation. |
| Documentation Package | Confirm that technical, quality, and shipping documents will be supplied in the required format and language. | Purchase order, approved drawings, project specifications, and agreed document requirements. | Drawing, material certificates, inspection report, coating report, test reports, certificate of conformity, packing list, and delivery records. | Documents should be complete, consistent, signed or electronically authorized, and available before final acceptance. | Conflicting quantities, inconsistent part numbers, missing revisions, or documents supplied only after repeated requests. |
| Pre-Shipment Verification | Arrange a production-line audit, remote inspection, or independent pre-shipment inspection before dispatch. | Customer inspection procedure and agreed acceptance criteria. | Inspection checklist, time-stamped photographs, sample measurements, packing inspection, and signed release report. | Inspection should cover quantity, dimensions, surface condition, markings, accessories, packaging, and document completeness. | Supplier refuses reasonable inspection, presents only selected samples, or changes the inspection date without explanation. |
| Packaging and Marking | Check protection against impact, moisture, thread damage, mixing of components, and loss of identification during transport. | Approved packaging specification and applicable transport requirements. | Packaging drawings, carton or bundle identification, product labels, moisture protection details, and loading photographs. | Every bundle or carton should show part number, quantity, batch reference, gross weight, and handling information where required. | Loose mixed parts, damaged threads, insufficient separation, illegible labels, or packaging that allows water accumulation. |
How to Choose the Best China Tower Clamp Supplier?
Price is only the opening point when comparing a China tower clamp supplier. Request itemized quotations for clamps, bolts, surface treatment, packaging, and transport. A low unit price may hide expensive tooling or inspection charges. Ask whether the quotation covers galvanized finish and export packing. In my experience, unclear pricing creates problems after approval. That lesson is easy to overlook.
Lead time should include production, quality checks, and port handling. Ask for a schedule with specific dates, not “fast delivery.” For example, 500 clamps may need three weeks for production and several days for inspection. Confirm the delivery port and holiday shutdowns. Delays happen. A supplier should explain risks before accepting your purchase order.
Customization requires practical engineering support. Share drawings, load requirements, steel grade, hole diameter, and coating thickness. Request a sample before mass production. Check dimensions with calipers and review the material certificate. Also examine order terms carefully. Discuss minimum order quantity, payment stages, replacement procedures, tolerances, and inspection rights. A written agreement is safer than friendly promises. I once underestimated packaging space, which increased freight costs. That mistake changed how I compare total order value.
Choosing a China tower clamp supplier requires more than comparing unit prices. Communication reveals engineering discipline. Ask whether the supplier confirms tower dimensions, steel grade, bolt class, coating, and load requirements in writing. Request a marked drawing before production. A vague answer is a warning.
Response speed also matters. McKinsey’s 2020 supply-chain survey found that 93% of leaders planned to increase resilience after major disruptions. Your supplier should provide a clear contact person, escalation route, and production updates. Ask for inspection photos, test records, and packing details. Short replies are convenient, but they can hide missing information. I have found that one unanswered technical question often becomes a costly installation delay.
Service continues after shipment. Check whether the warranty states coverage, duration, exclusions, and evidence requirements. It should explain who pays for replacement freight and how claims are handled. ISO’s 2023 Survey reported more than 1.2 million ISO 9001 certificates worldwide. Certification supports process control, but it does not prove every clamp is suitable for your tower. Request material certificates, batch traceability, dimensional inspection reports, and independent load-test evidence. Contact two recent customers, preferably on similar projects. Ask about response time after a defect, not only delivery speed. A supplier may promise everything during quotation. The real test comes when a bolt does not fit.
Whether you’re looking for fire-rated walls, doors, openings, floors or a specialty service, we have the solution for you. With over 40 years of experience in testing, innovating, and providing technologically advanced fire-rated glass and framing products, we deliver unyielding performance and quality at a competitive price.